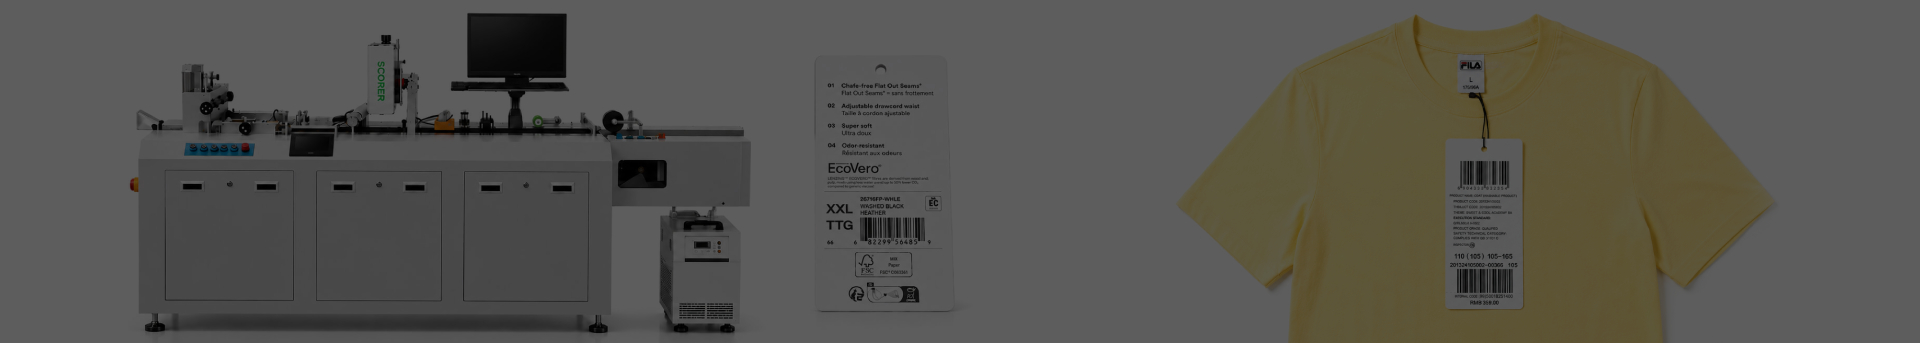
An RFID hang tag printer is a system that prints visible information on a hang tag and, when equipped with an RFID module, reads or encodes the chip inside it. An industrial system may also verify the printed image and RFID data, mark or reject defective tags, and record production results. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
The machine feeds each tag to a controlled position, reads the TID if required, writes the EPC or other authorized data, verifies the write result, and prints the corresponding text, barcode or QR code. Optional vision and RF inspection modules then check quality before the tag is collected or rejected. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Yes. A properly integrated print-and-encode system coordinates surface printing and chip encoding in one production workflow. "At the same time" usually means in one automated pass; the exact internal sequence may be read, write, verify and print. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
A regular label printer only produces visible text, graphics and barcodes. An RFID printer also communicates with the embedded chip, writes and verifies electronic data, and should handle failed encodings so that a good-looking tag with incorrect chip data is not released. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
An RFID encoder writes or reads chip data but may not print anything. An RFID printer/encoder combines visible printing with chip read/write and verification; an industrial line may additionally include feeding, curing, vision inspection and rejection. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
It may print on the surface if the material, ink adhesion and tag construction are suitable, but it cannot encode the RFID chip without an RFID read/write module and control software. Pressure, heat, static electricity and the raised inlay area must also be evaluated to avoid damaging tags or reducing print quality. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Import an approved data file or connect the software to a database, map fields such as SKU, serial number, barcode and EPC, then bind the print record to the RFID record. The system should validate formats, prevent duplicates, synchronize printing and encoding, and export an audit log. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Yes, if the RFID module, antenna arrangement, chip protocol and software support the required operation. TID is normally factory-programmed and read-only, while EPC memory is written according to the customer's encoding rules; sample validation is required before production. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes. The software can use one source record to generate the visible serial number, barcode or QR code and the related EPC. A robust workflow verifies both outputs and their association, rather than checking only print quality or only the chip. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes. Industrial variable-data inkjet systems can print changing QR codes, 1D barcodes, serial numbers, SKUs, text and graphics. Code type, minimum size, resolution, substrate and production speed should be tested together to ensure scanability. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Yes. The reader can read the programmed memory again and compare it with the intended value. For stronger quality control, verification can also include TID-EPC association, uniqueness, memory status and optional RF performance testing. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes, provided the software maintains a job-level or database-level uniqueness check and compares every read-back value with the source record. The handling rule should define whether the machine pauses, marks the tag, rejects it or records an exception. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes, with the appropriate detection and rejection configuration. Depending on the tag format and line design, failures may be physically rejected, separated, stopped for removal or visibly marked; the selected method must be confirmed during solution design. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Usually yes. Registration marks, tag size, coating, ink compatibility, inlay position, stack flatness and feeding reliability must first be checked. A sample run is essential because pre-print coatings and die-cut tolerances can affect adhesion and positioning. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
A machine can be engineered for UHF, NFC/HF or both, but these frequencies require different reader modules, antennas and protocols. Support should be confirmed by exact chip model and use case rather than assumed from the word "RFID." Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Many compatible chips support access passwords and permanent or reversible memory locks. Because an incorrect permanent lock cannot be undone, the memory map, password policy, authorization and verification procedure must be approved before production. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Basic read-back confirms data and tag response, but it is not the same as measuring RF performance. Sensitivity, tuning and operating-range tests require a dedicated RFID performance-testing module; define whether the requirement is data verification or true RF quality testing. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Speed must be stated under defined conditions: tag size, gap, print coverage, resolution, number of printheads, RFID operations and inspection configuration. Ask for both maximum mechanical speed and verified production output using your actual sample. Published speed is often a mechanical maximum measured under selected conditions. Actual good output is determined by tag length and gap, print resolution and coverage, the number of RFID commands, verification time, inspection modules, feeding stability, cleaning and job changeovers. Two machines with the same metres-per-minute figure may therefore produce very different numbers of accepted tags per hour. RFID operations can become the limiting station. Reading TID, writing a short EPC and verifying it requires less time than writing a larger memory block, applying a password, locking memory and repeating several verification cycles. If the line advances before communication is complete, failure rates rise even though the transport mechanism itself can run faster. For buyers, the most meaningful capacity figure is sustained accepted output using their own tags and data. It should be supported by the test duration, sample dimensions, chip/inlay model, print settings, first-pass yield, retry rate and final reject rate. A short video of peak speed cannot by itself prove industrial capacity.
Hourly output equals stable line speed converted by tag pitch, minus stops, rejects and changeovers. A useful quotation should show tested tags per minute or hour for the customer's size and encoding sequence, not only a theoretical peak. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Chip response time, memory volume, access password, lock commands, read-back cycles, antenna isolation, inlay spacing, RF power and failed-tag retries all affect speed. Printing resolution, UV curing and inspection can become additional bottlenecks. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes, if the system is configured for industrial feeding, continuous duty, stable data processing, consumable supply, inspection and failure handling. Capacity should be proven by an extended sample run that records uptime, good-output rate and encoding accuracy. Published speed is often a mechanical maximum measured under selected conditions. Actual good output is determined by tag length and gap, print resolution and coverage, the number of RFID commands, verification time, inspection modules, feeding stability, cleaning and job changeovers. Two machines with the same metres-per-minute figure may therefore produce very different numbers of accepted tags per hour. RFID operations can become the limiting station. Reading TID, writing a short EPC and verifying it requires less time than writing a larger memory block, applying a password, locking memory and repeating several verification cycles. If the line advances before communication is complete, failure rates rise even though the transport mechanism itself can run faster. For buyers, the most meaningful capacity figure is sustained accepted output using their own tags and data. It should be supported by the test duration, sample dimensions, chip/inlay model, print settings, first-pass yield, retry rate and final reject rate. A short video of peak speed cannot by itself prove industrial capacity.
There is no honest universal number because results depend on chip quality, inlay placement, RF settings, tag spacing and the definition of "success." Request test results showing first-pass yield, final yield after retry, reject rate and sample conditions. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
It can when RF isolation, antenna positioning, motion control and software timing are properly engineered. Stability should be validated at the target production speed using the actual inlay, including adjacent-tag interference and repeated start-stop tests. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Output per hour is strongly affected by tag length in the feed direction and the gap between tags. Very small, thick, warped or irregular tags may also require slower feeding to maintain separation, registration and reliable RFID positioning. Published speed is often a mechanical maximum measured under selected conditions. Actual good output is determined by tag length and gap, print resolution and coverage, the number of RFID commands, verification time, inspection modules, feeding stability, cleaning and job changeovers. Two machines with the same metres-per-minute figure may therefore produce very different numbers of accepted tags per hour. RFID operations can become the limiting station. Reading TID, writing a short EPC and verifying it requires less time than writing a larger memory block, applying a password, locking memory and repeating several verification cycles. If the line advances before communication is complete, failure rates rise even though the transport mechanism itself can run faster. For buyers, the most meaningful capacity figure is sustained accepted output using their own tags and data. It should be supported by the test duration, sample dimensions, chip/inlay model, print settings, first-pass yield, retry rate and final reject rate. A short video of peak speed cannot by itself prove industrial capacity.
Yes. Digital inkjet printing does not require physical printing plates, so artwork and variable-data jobs can be changed through software. Operators still need to load and validate the new file, adjust media settings where necessary, and perform a first-piece check. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Compatibility must be confirmed against the exact chip, inlay design, frequency, memory map and tag construction. Suppliers should run samples because two tags using the same IC can behave differently when antenna geometry and placement change. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Common UHF chips from these suppliers may be supported when they follow the required protocol, but brand-level confirmation is insufficient. Provide the exact IC and inlay model, memory requirement and commands so read, write, lock and verification functions can be tested. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
The answer depends on the installed module. For apparel UHF projects, buyers commonly request EPC Class 1 Gen 2 / ISO 18000-63 compatibility; NFC/HF projects use different ISO standards. The quotation should list the exact supported protocol and regional frequency. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
The usable range depends on feeder width, transport platform, sensor position, tag thickness and inlay layout. Confirm minimum and maximum width and length, but also test the smallest, largest and most difficult real samples. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
GSM alone is not enough because equal-GSM materials can have different thickness, stiffness, coating and friction. Provide GSM, measured thickness, dimensions, surface treatment, inlay position and stacked samples for a reliable feeding test. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Often yes with the correct ink and curing settings. Adhesion, dot gain, barcode contrast, scratch resistance and any surface treatment should be tested because "coated paper" and "synthetic paper" cover many different materials. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Yes, a sheet-fed platform can be designed for individual die-cut tags. Feeding reliability depends on clean edges, consistent stacks, static control, holes, strings, embossing, warpage and inlay bulges, so sample testing is mandatory. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Possibly, if the feeder and transport system can separate, guide and register the shape consistently. The supplier should evaluate the outline, center of gravity, leading edge, holes, thickness and printable area before confirming. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Yes within the antenna's adjustable or multi-station operating range, but each layout may require a recipe for encoding position, RF power and timing. Widely separated or unusual positions may require hardware adjustment or additional antennas. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Usually yes. Changing the inlay, tag pitch, thickness or antenna position can change the optimum encoding point and power. Save validated recipes for repeat jobs and run a first-piece read/write/print check after every material change. Media compatibility has three separate dimensions: the tag must feed mechanically, accept the ink and communicate reliably by RFID. A material can pass one test and fail another. For example, a coated card may print well but slip during feeding, while a thick inlay may feed correctly but create an uneven printing gap. GSM describes weight per unit area, not the complete behaviour of a tag. Thickness, stiffness, surface friction, coating, static electricity, die-cut quality, holes, curvature and the raised inlay area all influence separation and registration. Chip brand alone is also insufficient because antenna geometry and inlay placement can change RF behaviour even when the same IC is used. Compatibility should therefore be understood as an approved combination of material construction, tag dimensions, chip/inlay and machine settings. When any of these changes, feeding, adhesion and RFID calibration may need to be checked again. Representative physical samples provide much more reliable evidence than a material name alone.
Industrial systems normally use job-design and production-control software that imports artwork and variable data, controls printing and RFID commands, verifies results and creates logs. Compatibility with existing label software or a customer database should be checked through the required interface and data workflow. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Most variable-data systems can import CSV and may support Excel directly or after conversion. Before production, define column names, encoding, leading zeros, data types, record count, duplicate rules and the mapping between printed and RFID fields. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Yes when the required API, database, file exchange or middleware interface is developed and authorized. Integration scope should specify who creates EPCs, who releases jobs, how results are returned, error handling, cybersecurity and acceptance testing. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
The software can serialize EPCs according to an approved rule, but uniqueness must be governed by the customer's numbering authority and database. The system should reserve ranges, prevent reuse, validate length and report consumed, rejected and unused codes. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Use the applicable GS1 EPC Tag Data Standard and identify the company prefix, item reference, serial number, filter value, partition and available chip memory. Do not simply copy a barcode string into EPC memory; validate the encoding scheme with the brand owner or GS1 specialist. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes. The production software can receive or query records, map fields into a template and issue one synchronized print-and-encode transaction per tag. Access control, caching, network interruption and record-status updates must be defined for production reliability. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Yes. A useful report can include job ID, time, operator, source record, TID, intended and read-back EPC, print inspection result, reject reason and totals. Confirm required format, retention period and whether sensitive data must be masked. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Yes if each job has a unique batch identifier and every tag result is logged against it. The batch report should reconcile input records, good output, retries, rejects, reprints and unused codes so quantities remain auditable. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
It can be configured to support relevant EPC schemes, but "GS1 compatible" should be demonstrated with the customer's real company prefix and encoding rule. Confirm scheme, bit length, partition, serialization and validation output before approval. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes through input validation, database uniqueness checks, range reservation and status control. It should also prevent an automatic retry or reprint from accidentally consuming or duplicating a code and flag duplicates found during read-back. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Price varies widely with sheet-fed or roll-to-roll format, print width and heads, RFID stations, vision inspection, rejection, RF performance testing, software integration and service. A meaningful quotation requires samples, size range, output target, data workflow and required modules. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
The best choice depends on the incoming format and production model. A sheet-fed system suits individual pre-die-cut hang tags, while roll-to-roll equipment suits continuous labels; compare real throughput, data integrity, changeover time, inspection and total cost rather than brand alone. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Buy from a manufacturer or authorized integrator that can test your tags, document compatibility, explain the data workflow and provide installation and service. Ask for a live sample test, configuration list, acceptance criteria, references and written warranty before ordering. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
When evaluating a Chinese manufacturer, verify whether it builds the complete print-and-encode system or only resells a desktop printer. Review factory capability, RFID and software engineering, sample-test reports, export experience, English documentation, spare-parts plan and remote/on-site support. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
A qualified supplier should ask about tag structure, chip, inlay position, artwork, EPC rules, volume and system interface before quoting. Suppliers who quote only from a product name may omit critical feeding, RF isolation, inspection or data-integration requirements. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Clarify whether the price is for a desktop thermal printer, a sheet-fed industrial inkjet line or a roll-to-roll production system. Compare included reader stations, software, curing, inspection, rejection, training, freight, installation, consumables and taxes on the same basis. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Before selecting a listed machine, submit representative samples and a written user requirement specification. Purchase approval should be based on a witnessed test and agreed acceptance criteria, not only catalog speed or demonstration material selected by the seller. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
A complete quotation should state the workflow, model, standard and optional modules, supported sample range, tested capacity, utilities, software scope, delivery, installation, training, warranty, consumables, exclusions and payment terms. Request a layout and process description as attachments. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
At minimum: feeder/unwinder, transport, inkjet system, curing, RFID read/write modules, control software, inspection/rejection options, computer, accessories, training and warranty. Also list what is excluded so the buyer can calculate the complete installed cost. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Calculate ink and cleaning fluid, labor, electricity, rejects, maintenance, depreciation, software/service and changeover waste. Chip and tag-stock cost should be shown separately; divide total production cost by verified good output, not by gross input quantity. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Ink consumption depends on printed area, coverage, resolution, grayscale, artwork and cleaning. The reliable method is to RIP the actual file or run a measured sample job, then report ink per 1,000 tags with the test conditions. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Compare annual in-house cost with outsourcing and existing labor, including plates, minimum-order charges, inventory, lead time, waste, rework and lost urgent orders. Add the value of faster changeovers, short runs, data control and reduced errors, then calculate payback from verified monthly savings. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Outsourcing avoids capital investment and may suit low or irregular volume, but adds supplier margin, minimum quantities, transport, lead time and data-sharing risk. In-house production offers faster response and control but requires equipment utilization, trained operators, maintenance and quality systems. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Typical requirements include stable power and grounding, adequate space, suitable temperature and humidity, ventilation for the ink/curing system, network access, material storage and safe operator access. Final requirements depend on the selected configuration and must be supplied in a pre-installation checklist. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Many industrial suppliers offer overseas installation as a paid or negotiated service. Confirm travel, visa, accommodation, local transport, installation days, interpreter, tools, customer responsibilities and what happens if the site is not ready. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Training should cover job setup, data import, printing, RFID recipes, first-piece approval, error handling, cleaning, preventive maintenance and backup. Confirm trainee number, language, duration, materials and whether competency or acceptance is documented. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Warranty duration and starting date must be stated in the contract, together with covered parts, exclusions, labor, travel and shipping. Consumables and damage caused by unapproved ink, improper operation or site conditions are commonly treated separately. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Operators normally perform daily or shift-based cleaning and checks, while filters, pumps, belts, lamps and motion parts follow usage-based schedules. The supplier should provide daily, weekly, monthly and annual maintenance lists matched to the installed system. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Follow the manufacturer's approved purge, wipe and capping procedure using specified cleaning fluid and lint-free materials. Never scrape the nozzle plate, use unapproved solvent or leave a UV printhead exposed to curing light; operator training is essential. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Confirm whether stock is held by a local distributor or shipped internationally, typical lead time, shelf life and minimum order. Keep a recommended critical-spares kit and sufficient approved ink and cleaning fluid based on consumption and shipping time. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Remote support can include video calls, secure remote diagnostics, log review, software guidance and operator coaching. Confirm service hours, language, response targets, connectivity/security rules and escalation to on-site service when remote recovery is insufficient. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Yes, and it is strongly recommended. Send representative good and difficult samples, artwork, variable-data files, chip/inlay details, required speed and acceptance criteria; request returned samples, a production video and a written result report. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
A serious supplier should provide videos and reports relevant to the proposed configuration and, ideally, the buyer's samples. The report should show setup, sample identity, speed, quantity, print quality, encoding verification, rejects and any limitations - not only a short edited clip. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Viewers want an uncut view of feeding, printing, RFID read/write, verification and output collection. Show the control screen and final tags, and state tag size and real operating speed. People use this search because static specifications cannot prove that the complete process works. They want to see how material enters the machine, how data is loaded, how printing and RFID operations are synchronized and what happens to the finished tags. A useful demonstration identifies the sample size, material, chip/inlay, print settings and real running speed. It shows continuous operation, the software screen and live counters rather than only close-up beauty shots. When data integrity is the subject, the video should also show the source record and the read-back result. The strongest evidence includes an intentional failure. Showing how the machine detects, marks or rejects a bad tag explains the control logic far better than claiming a perfect success rate. Independent barcode scanning and RFID reading of finished samples make the result easier for buyers to trust.
Demonstrate one complete data record moving from the source file to the printed tag and encoded chip. Read the finished tag with an independent reader to prove the result. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Use real apparel hang tags and show short-run changeover, variable SKU data and barcode scanning. Buyers need to see stable feeding of die-cut tags, not only a generic adhesive label. People use this search because static specifications cannot prove that the complete process works. They want to see how material enters the machine, how data is loaded, how printing and RFID operations are synchronized and what happens to the finished tags. A useful demonstration identifies the sample size, material, chip/inlay, print settings and real running speed. It shows continuous operation, the software screen and live counters rather than only close-up beauty shots. When data integrity is the subject, the video should also show the source record and the read-back result. The strongest evidence includes an intentional failure. Showing how the machine detects, marks or rejects a bad tag explains the control logic far better than claiming a perfect success rate. Independent barcode scanning and RFID reading of finished samples make the result easier for buyers to trust.
Show antenna setup, TID reading, EPC writing, read-back verification and failure handling. State the chip/inlay model and regional frequency used in the test. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Display the source record, captured TID, intended EPC and verified EPC side by side. Include the production log so viewers can see the association is stored. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Explain that print verification and RFID verification are separate checks, then demonstrate both. Include how the machine reacts when either check fails. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Use a wide shot and continuous counter to prove sustained output. Publish test conditions and good-output rate instead of showing only a few seconds at maximum speed. Published speed is often a mechanical maximum measured under selected conditions. Actual good output is determined by tag length and gap, print resolution and coverage, the number of RFID commands, verification time, inspection modules, feeding stability, cleaning and job changeovers. Two machines with the same metres-per-minute figure may therefore produce very different numbers of accepted tags per hour. RFID operations can become the limiting station. Reading TID, writing a short EPC and verifying it requires less time than writing a larger memory block, applying a password, locking memory and repeating several verification cycles. If the line advances before communication is complete, failure rates rise even though the transport mechanism itself can run faster. For buyers, the most meaningful capacity figure is sustained accepted output using their own tags and data. It should be supported by the test duration, sample dimensions, chip/inlay model, print settings, first-pass yield, retry rate and final reject rate. A short video of peak speed cannot by itself prove industrial capacity.
Deliberately introduce a failed tag and show detection, alarm, marking/rejection and log entry. This proves that failures are controlled rather than silently passed downstream. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Show consecutive tags with changing QR codes, barcodes, serial numbers and SKUs, then scan several outputs. Explain how records are imported and mapped. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Demonstrate that the QR/barcode content and EPC belong to the same source record. Visual code scanning plus RFID read-back makes the relationship easy to understand. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Cover material loading, sensor and print-position setup, RFID recipe selection, test print, read/write verification and first-piece approval. Avoid exposing passwords or confidential customer data. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Teach job creation, artwork import, variable-field mapping, EPC rule setup, duplicate checks, preview, production and report export. Use dummy data and divide the tutorial into short chapters. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Check tag quality, inlay position, antenna alignment, RF power, tag pitch, protocol, memory settings and passwords in a safe sequence. Show diagnosis rather than merely increasing RF power. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Show approved daily cleaning, nozzle check, capping, filter/consumable checks and safe shutdown. Separate operator maintenance from procedures reserved for trained service engineers. Industrial RFID inkjet equipment is a production system rather than a simple office appliance. Stable power and grounding, suitable temperature and humidity, ventilation, network access, material storage and sufficient operating space affect reliability. Some configurations also require compressed air or specific exhaust arrangements. Installation normally includes mechanical positioning, utility connection, printhead and curing setup, RFID calibration, software configuration, sample testing and operator training. Training should explain normal operation as well as cleaning, first-piece approval, error handling, backup and preventive maintenance, because many avoidable failures originate in daily operation. Service capability should be judged by response process, spare-parts availability and technical competence, not only by the warranty period. Remote diagnosis can solve software and setup issues quickly, while physical failures may require replacement parts or on-site service. Clear responsibilities and records reduce downtime after delivery.
Show the complete workflow from blank or pre-printed tags to data import, printing, encoding, inspection, rejection and finished collection. Add a simple process overlay and production statistics. Published speed is often a mechanical maximum measured under selected conditions. Actual good output is determined by tag length and gap, print resolution and coverage, the number of RFID commands, verification time, inspection modules, feeding stability, cleaning and job changeovers. Two machines with the same metres-per-minute figure may therefore produce very different numbers of accepted tags per hour. RFID operations can become the limiting station. Reading TID, writing a short EPC and verifying it requires less time than writing a larger memory block, applying a password, locking memory and repeating several verification cycles. If the line advances before communication is complete, failure rates rise even though the transport mechanism itself can run faster. For buyers, the most meaningful capacity figure is sustained accepted output using their own tags and data. It should be supported by the test duration, sample dimensions, chip/inlay model, print settings, first-pass yield, retry rate and final reject rate. A short video of peak speed cannot by itself prove industrial capacity.
Choose by media format, tag size, volume, print content, chip, verification requirement and integration - not by a universal ranking. Test actual tags on sheet-fed and roll-to-roll candidates when both formats are possible. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Ask users about sustained throughput, feeding stability, nozzle maintenance, ink adhesion, EPC accuracy, changeover time and after-sales response. A useful reference should use similar tags and production volume. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Use a plate-free variable-data workflow with saved templates and RFID recipes. Prepare validated data, run a first-piece check, print only the required quantity and reconcile every good, rejected and unused code. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Control EPCs centrally, reserve unique ranges, validate imports, block previously used values and manage retries/reprints transactionally. Read-back verification and final batch reconciliation provide a second line of defense. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Generate both from one database record and assign a unique internal record ID. After printing and encoding, scan/read both outputs and compare them against the same record before accepting the tag. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Thermal transfer is common for narrower labels and established ribbon workflows; UV inkjet can suit high-speed, wide or plate-free variable printing on compatible materials. Compare resolution, durability, width, throughput, consumables, media heat sensitivity and total cost using real samples. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Read back every programmed tag, apply a defined retry limit, then mark, reject or stop on persistent failure. Log the TID, intended EPC, error reason and disposition, and ensure any replacement tag receives the correct controlled code. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Yes, an integrated industrial line can coordinate these modules. Confirm whether inspection covers only print, RFID data read-back, or true RF performance, and confirm the physical reject method for the customer's tag format. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Look for engineering depth, factory testing, transparent limitations, documented acceptance criteria, export references, software capability and long-term consumables/service support. Verify claims with your samples and a live witnessed test. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
The range is much broader than desktop printer pricing because an industrial solution may include feeding, multiple heads, curing, several RFID stations, inspection, rejection and integration. Define scope first and compare total installed cost. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
High-speed success depends on RF isolation and process control as much as reader specifications. Ask for long-run results, first-pass yield, adjacent-tag interference testing, failure recovery and actual inlay details. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Send tag photos and samples, dimensions, thickness/GSM, chip and inlay position, incoming format, print artwork, variable-data and EPC rules, required output, inspection, system interface, destination and service expectations. This prevents an incomplete or misleading quotation. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
For individual pre-die-cut hang tags, start with a sheet-fed industrial inkjet print-and-encode system; for continuous label stock, evaluate roll-to-roll. Require TID reading, EPC writing and read-back, synchronized variable printing, duplicate control, optional vision/RF inspection, failure handling and sample-proven feeding. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Use an integrated RFID variable-data printing system with a database-driven controller. It should capture TID, create or receive the authorized EPC, print the QR code from the same record, read back the chip and store the association before accepting the tag. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Use digital inkjet templates and imported variable-data files instead of physical plates. Save material and RFID recipes, perform automated print/encode verification, and use quick first-piece approval so small jobs can change with limited setup waste. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Sheet-fed machines suit separate, pre-die-cut hang tags and flexible short runs but depend heavily on stack feeding. Roll-to-roll machines suit continuous labels and automated winding with higher continuous efficiency, but require compatible roll construction and may involve more setup; choose by incoming and required finished format. This question should be considered from the complete production workflow, not from one isolated function. The incoming tag format, visible print, electronic data, inspection method and required finished form must work together. A technically possible function may still be unsuitable for production if feeding is unstable, data cannot be traced or changeover takes too long. The practical answer therefore depends on the customer's actual samples, order pattern and quality requirements. The most reliable understanding comes from a sample test that reproduces the intended job. It should show not only that the machine can complete the task once, but that it can repeat it consistently while recording and controlling exceptions.
Check actual manufacturer status, sample compatibility, tested output and yield, RFID protocol and chip support, data security, inspection/rejection scope, software integration, configuration and exclusions, installation, training, warranty, parts, ink supply and references. Put acceptance criteria in the contract. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Add tag stock and chip, ink and cleaning fluid, labor, power, rejects, maintenance, software/service, depreciation and changeover waste. Divide by accepted good tags and model several utilization levels; separate equipment payback from per-job cash cost. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Choose an integrated system with post-write read-back, source-data comparison, duplicate checking and a physical rejection or marking module. Ask the supplier to demonstrate an intentionally incorrect or unreadable tag and show the corresponding log. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Yes through an agreed API, database connection, middleware or controlled file exchange. First define the data owner, job-release logic, field mapping, acknowledgements, error/retry behavior, security, offline operation and return of production results. The software is the link between the customer's business data and the physical tag. It receives or generates records, maps fields to the artwork and RFID memory, sends synchronized commands to the machine and records the result. If field definitions or serialization rules are wrong, the machine can reproduce the error perfectly at high speed. File support does not only mean that a file can be opened. The system must preserve leading zeros, character encoding, field length, record order and uniqueness, and it must handle missing or invalid values. ERP or database integration also requires clear ownership of EPC creation, job release, acknowledgements, retries and status return. Traceability means that the factory can later identify what happened to every record in a batch. A complete log may contain the job and time, source record, TID, intended and verified EPC, printed-code inspection, retry or rejection reason and reprint status. This information allows production totals and customer data to be reconciled.
Use a plate-free digital inkjet system with template management, database import, automated serialization, RFID synchronization, duplicate prevention and inspection. Organize jobs by SKU and saved recipes while keeping a single controlled source of truth for data. RFID printer pricing cannot be compared accurately until the equipment category is clear. A desktop thermal printer, a sheet-fed industrial inkjet system and a roll-to-roll production line solve different production problems. Their prices may include very different feeding, printing, curing, RFID, inspection, rejection and software functions. The final configuration is driven by the customer's tag format, dimensions, substrate, chip/inlay, print width and coverage, required output, encoding rules, inspection level and connection to other systems. Optional modules can materially change both investment and operating cost, so a low headline price may exclude functions that are essential to the project. A proper commercial comparison uses total installed cost and verified good output. Buyers should include equipment, software, freight, installation, training, ink, cleaning fluid, spare parts, labor, rejects, maintenance and downtime. Return on investment is created not only by lower unit cost, but also by shorter lead time, fewer plates, less inventory, faster replenishment and better data control.
Generate both values from one validated record, assign a transaction ID, print and encode under the same transaction, then scan the barcode and read back the EPC. Accept the tag only when both match the expected record; log and reject any mismatch. The important point is that RFID processing is an electronic data operation, not merely a printing operation. TID normally identifies the chip itself, while EPC normally identifies the item represented by the tag. The software must therefore know which memory bank is being accessed, what data format is permitted and whether the data is read-only, writable, password-protected or lockable. Reliable encoding also depends on physical RF conditions. The position and design of the inlay antenna, the gap between adjacent tags, reader-antenna alignment, write power and line speed can change the result. Excessive power may activate a nearby tag, while insufficient power may cause intermittent failures. This is why the same settings cannot automatically be applied to every RFID hang tag. In real production, a successful write command is not enough. The system should read the value back, compare it with the intended record and retain the relationship among the source data, TID, EPC and visible code. Failed, repeated or mismatched records must be identified so that a visually correct tag with incorrect electronic data is not delivered.
Actual performance depends on tag size, material, chip and inlay design, data volume, print coverage, resolution, inspection configuration and operating environment. Samples should be tested before final configuration and quotation.